
How to Verify CNC Part Quality Before Production: CMM Inspection Standards and Supplier Evaluation Guide
Ningbo, Zhejiang, China – October 10, 2026
Quick read:
- Pre-production CNC quality verification is an 8-step framework that runs from the 2D / 3D drawing review through the first-article CMM inspection report, with the CMM (coordinate measuring machine) being the single most documentable artifact.
- The five standards that anchor a compliance-grade supplier’s quality envelope are ISO 9001:2015 (quality management), ISO 13485:2016 (medical device), IATF 16949:2016 (automotive), ASME Y14.5 (GD&T), and ISO 2768-1 (general tolerance).
- The CMM accuracy envelope is the difference between a “we have a CMM” supplier and a “we have a calibrated, traceable CMM” supplier: ISO 10360 defines the accuracy class, and the supplier’s calibration certificate is dated within the last 12 months.
- First-article inspection is the single document that separates a destination-port-pass order from a destination-port-reject order, and a PPAP-style first-article report is the procurement reference for an automotive, medical, or aerospace tier-1 customer.
Why Pre-Production CNC Quality Verification Matters Before Cutting Steel
A custom CNC machined part is, by definition, a part that has never been made before. The buyer’s engineering team releases a 2D or 3D drawing to the supplier, the supplier’s engineering team reviews the drawing for manufacturability, the supplier cuts a prototype or a first-article sample on the CNC machine, and the supplier’s quality team inspects the sample on the CMM. The first-article inspection is the document that the buyer’s quality team checks before authorizing the production batch, and the first-article inspection report is the document that the buyer’s destination-port quality team checks when the production batch lands at the buyer’s warehouse.
The cost of skipping the pre-production quality verification is concentrated in three failure modes. The first failure mode is a drawing-review miss: the supplier cuts a 50-piece prototype to a 2D drawing that has a missing GD&T callout, the prototype passes the supplier’s in-house inspection on a hand caliper, and the production batch fails the buyer’s CMM inspection because the GD&T envelope was never validated at the drawing-review stage. The second failure mode is a tool-path miss: the supplier’s CAM engineer programs a 3-axis tool path for a 5-axis feature on the drawing, the production batch cuts the feature in two set-ups instead of one, and the cumulative tolerance stack exceeds the drawing envelope by 0.05 mm. The third failure mode is a CMM-program miss: the supplier inspects the first-article on a CMM that has a 5-year-old calibration certificate, the CMM drift envelope is 0.02 mm, and the production batch’s first-article report shows a 0.02 mm error that the buyer’s quality team catches at the destination port.
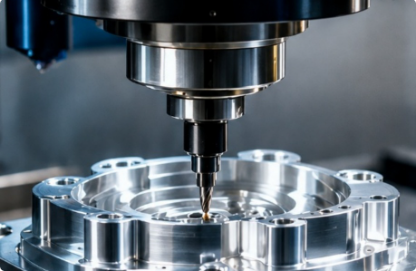
The pre-production quality verification framework below is built around the CNC Milling Service envelope at FRIMA and the quality-control envelope that documents the CMM and traceability stack. The 8-step framework is the procurement reference that an OEM or a tier-1 supplier applies before authorizing a 50-piece to 5,000-piece production batch of a custom machined part or a special-drawing assembly. The destination for the framework is the engineering team and the quality team at the buyer, and the framework’s deliverable is a documented first-article CMM inspection report that the buyer’s quality team can accept at the destination port without re-inspection.
Step 1: 2D / 3D Drawing Review and Manufacturability Feedback
The first step in the pre-production quality verification framework is the 2D / 3D drawing review, and the deliverable from the review is a documented manufacturability report that lists the dimensions, tolerances, GD&T callouts, surface-finish callouts, material callouts, and any feature that is at risk of falling outside the drawing envelope at the production-batch stage. The drawing review is the cheapest step in the framework and the step that catches the most expensive downstream errors, and a supplier that does not return a documented drawing review within 24 hours of receiving a 2D / 3D drawing is a supplier that has not invested in the engineering discipline that the buyer’s quality team requires.
The drawing-review deliverable includes the manufacturability assessment (what features can be cut on a 3-axis machine, what features require a 5-axis machine, what features require a lathe + milling set-up), the tolerance-stack assessment (which dimensions are the critical-to-quality dimensions, which dimensions are the non-critical reference dimensions), the surface-finish assessment (which surfaces require a Ra callout, which surfaces are non-critical), the material assessment (which material grades are stocked, which material grades require a special order), and the first-article inspection plan (which dimensions will be measured on the CMM, which dimensions will be measured on a hand caliper, which dimensions will be measured on a surface-finish tester). A supplier that returns all five sections of the manufacturability report is a supplier that has invested in the engineering discipline, and a supplier that returns only a price quote without a manufacturability report is removed from the comparison.
The drawing review is the first opportunity for the buyer’s engineering team to flag a GD&T callout that the supplier’s engineering team has read differently. The ASME Y14.5 standard defines the GD&T envelope for machined parts, and a supplier that has an ASME Y14.5-trained engineering team is the supplier that the buyer’s engineering team shortlists. A supplier that does not have an ASME Y14.5-trained engineering team is a supplier that will read a GD&T callout literally, and the literal reading will produce a part that fails the buyer’s functional-test envelope at the production-batch stage.
Step 2: Material Certification and Incoming Material Inspection
The second step is the material certification and incoming material inspection, and the deliverable from this step is a mill test certificate (MTC) for the raw material lot that the supplier will cut into the production batch. The MTC documents the material grade, the heat-treatment condition, the chemical composition, the mechanical properties, and the traceability back to the mill that produced the raw material. The MTC is the document that the buyer’s quality team checks at the destination port, and an MTC that is missing or that is dated before the supplier’s material order is an MTC that fails the buyer’s quality envelope.
The incoming material inspection is the supplier’s in-house verification that the MTC matches the actual material that arrives at the supplier’s incoming-inspection bench, and the inspection typically includes a dimensional check (the bar stock diameter or the plate thickness is within the MTC envelope), a visual check (no surface defects, no scale, no oxidation), and a hardness check (the as-delivered hardness is within the MTC envelope, and the post-heat-treatment hardness will be within the drawing envelope). A supplier that returns a documented MTC plus a documented incoming-inspection report is the supplier that the buyer’s quality team shortlists, and a supplier that returns only the MTC without an incoming-inspection report is a step behind on the material-certification envelope.
The traceability envelope is the third component of the material-certification step, and the deliverable from the traceability envelope is a documented chain of custody from the mill to the supplier’s incoming-inspection bench to the supplier’s CNC machine to the supplier’s CMM to the supplier’s shipping dock. The traceability chain is the document that the buyer’s quality team uses to recall a specific production batch in the event of a destination-port failure, and a supplier that cannot return a documented traceability chain is a supplier that cannot support a recall. The ISO 9001:2015 quality management standard defines the traceability envelope, and a supplier that has a current ISO 9001:2015 certificate is the supplier that has invested in the traceability envelope.
Step 3: Tooling, Fixture, and Work-Holding Strategy
The third step is the tooling, fixture, and work-holding strategy, and the deliverable from this step is a documented tooling plan that lists the cutting tools (end mills, drills, taps, reamers, inserts), the work-holding fixtures (vises, chucks, soft jaws, custom fixtures), and the set-up sequence (which features are cut in which set-up, which fixtures are used in which set-up). The tooling plan is the document that the buyer’s engineering team uses to assess the supplier’s manufacturing maturity, and a supplier that returns a documented tooling plan with tool-by-tool and fixture-by-fixture detail is a supplier that has invested in the manufacturing-maturity envelope.
The tooling-plan detail includes the cutting-tool material (carbide, ceramic, diamond-coated), the cutting-tool geometry (number of flutes, helix angle, corner radius), the cutting parameters (spindle speed, feed rate, depth of cut, step-over), and the tool-life envelope (the expected number of parts per tool, the tool-replacement schedule). A supplier that returns all four components of the tooling-plan detail is the supplier that has invested in the manufacturing-maturity envelope, and a supplier that returns only a generic “we will use carbide end mills” is a step behind.
The work-holding strategy is the second component of the tooling-plan envelope, and the work-holding strategy includes the fixture type (standard vise, custom soft-jaw, vacuum chuck, magnetic chuck), the work-holding pressure (clamping force in N or kgf), the work-holding distortion envelope (the maximum distortion of the part at the clamping point), and the set-up sequence (which surfaces are referenced for the datum envelope). A supplier that returns all four components of the work-holding strategy is the supplier that has invested in the work-holding envelope, and a supplier that returns only “we will use a vise” is a step behind on the work-holding envelope. The work-holding strategy is particularly critical for thin-wall parts, soft-material parts (aluminum, brass, copper), and high-tolerance parts where the clamping distortion is a measurable percentage of the drawing tolerance.
Step 4: CNC Machine-Tool Envelope and Calibration
The fourth step is the CNC machine-tool envelope and the machine-tool calibration, and the deliverable from this step is a documented machine-tool inventory (the CNC machines in the supplier’s production floor, the machine-tool brands, the machine-tool ages, the machine-tool axis counts) and a documented machine-tool calibration record (the most recent ballbar test, the most recent laser calibration, the most recent servo-tuning record). The machine-tool inventory is the document that the buyer’s engineering team uses to assess the supplier’s capacity envelope, and the machine-tool calibration is the document that the buyer’s quality team uses to assess the supplier’s precision envelope.
A CNC machine-tool inventory that includes 3-axis vertical machining centers, 5-axis vertical machining centers, CNC lathes, and CNC turning-milling centers is a complete inventory for a custom-machined-parts supplier, and an inventory that includes only 3-axis machines is an inventory that cannot support 5-axis features on a drawing. A supplier with 5 or more 5-axis machines is a supplier that has invested in the 5-axis envelope, and a supplier with 1 or 2 5-axis machines is a step behind on the 5-axis envelope. The machine-tool age is the second component of the inventory envelope, and a supplier with machines that are 5 years old or newer is a supplier that has invested in the machine-tool envelope, and a supplier with machines that are 10 years old or older is a step behind on the machine-tool envelope.
The machine-tool calibration record is the second component of the step, and the calibration record includes the ballbar test (a circularity test that measures the machine’s geometric accuracy, with a pass criterion of less than 0.01 mm at 300 mm/s), the laser calibration (a linear-positioning test that measures the machine’s axis-positioning accuracy, with a pass criterion of less than 0.005 mm at full travel), and the servo-tuning record (a dynamic-response test that measures the machine’s contouring accuracy, with a pass criterion of less than 0.01 mm at the rated feed rate). A supplier that returns all three calibration records dated within the last 12 months is the supplier that has invested in the calibration envelope, and a supplier that returns only the ballbar test is a step behind on the calibration envelope. The NIST machine-tool calibration traceability is the metrology reference for the ballbar test and the laser calibration, and a supplier that returns a NIST-traceable calibration certificate is the supplier that has invested in the metrology envelope.
Step 5: CMM Inspection Envelope and ISO 10360 Accuracy
The fifth step is the CMM inspection envelope and the ISO 10360 accuracy class, and the deliverable from this step is a documented CMM inventory (the CMM brands, the CMM ages, the CMM axis counts, the CMM probing systems) and a documented ISO 10360 accuracy certificate (the most recent accuracy test, the most recent probe calibration, the most recent ball-plate verification). The CMM is the single most documentable artifact in the pre-production quality verification framework, and a supplier that has a calibrated, traceable CMM is a supplier that has invested in the inspection envelope.
The CMM inventory includes the CMM brand (Zeiss, Renishaw, Hexagon, Mitutoyo are the four tier-1 brands), the CMM age (a CMM that is 5 years old or newer is current-generation, a CMM that is 10 years old or older is a step behind), the CMM axis count (a 3-axis CMM is standard, a 5-axis CMM is required for complex geometries), and the probing system (a touch-trigger probe is standard, a scanning probe is required for complex surface inspections, a vision probe is required for small-feature inspections). A supplier that returns a tier-1 brand CMM with a 5-axis configuration and a scanning probe is the supplier that has invested in the CMM envelope. The Renishaw CMM probing and inspection reference and the Mitutoyo CMM inspection reference are the metrology-industry references for the CMM probing envelope, the probe-calibration envelope, and the CMM program envelope, and a supplier that documents the CMM envelope against the Renishaw or Mitutoyo reference is the supplier that has invested in the metrology discipline.
The ISO 10360 accuracy certificate is the second component of the step, and the ISO 10360 standard defines the CMM accuracy envelope as the maximum permissible error (MPE) at a specific length. The typical ISO 10360 accuracy class for a tier-1 CMM is MPE = 1.5 + L/333 μm (where L is the measured length in mm), and a supplier that returns an ISO 10360 certificate dated within the last 12 months is the supplier that has invested in the CMM accuracy envelope. A supplier that returns only a “CMM calibration” without an ISO 10360 certificate is a step behind on the CMM envelope, and the buyer should request the ISO 10360 certificate as a procurement requirement.
Step 6: First-Article Inspection Report (PPAP-Style)
The sixth step is the first-article inspection report, and the deliverable from this step is a documented first-article report that lists every dimension on the drawing, the nominal value, the tolerance envelope, the measured value, the pass/fail status, and the CMM program that produced the measured value. The first-article report is the document that the buyer’s quality team checks at the destination port, and a first-article report that is missing dimensions, that has unmeasured dimensions, or that has pass/fail status without a CMM program reference is a first-article report that fails the buyer’s quality envelope.
A PPAP-style first-article report is the procurement reference for an automotive, medical, or aerospace tier-1 customer, and the PPAP (production part approval process) standard is the AIAG reference for the automotive industry. A PPAP-style report includes the dimensional inspection report (every dimension on the drawing, measured on the CMM, with a pass/fail status), the material certification (MTC + incoming-inspection report), the functional test report (if the part has a functional requirement, the test method, the test result, the pass/fail status), the appearance report (if the part has an appearance requirement, the visual inspection, the pass/fail status), and the control plan (the supplier’s process-control plan for the production batch). A supplier that returns all five sections of the PPAP-style report is the supplier that has invested in the first-article envelope, and a supplier that returns only the dimensional inspection report is a step behind on the first-article envelope.
The first-article report is the single document that separates a destination-port-pass order from a destination-port-reject order, and the procurement team should require the first-article report as a contractual deliverable for every custom machined part or special-drawing assembly. The first-article report is the document that the supplier’s quality team generates after the first-article sample is cut, and the first-article report is the document that the buyer’s quality team checks before authorizing the production batch. A supplier that cannot return a first-article report within 5 business days of the first-article sample being cut is a supplier that has not invested in the first-article envelope.
Step 7: In-Process Inspection and Statistical Process Control (SPC)
The seventh step is the in-process inspection and statistical process control (SPC), and the deliverable from this step is a documented in-process inspection plan (which dimensions are measured during the production batch, the inspection frequency, the inspection tooling) and a documented SPC envelope (the control charts, the Cpk values, the out-of-control action plan). The in-process inspection is the production-batch-level envelope that catches the dimension drift that a first-article-only envelope would miss, and the SPC envelope is the production-batch-level documentation that the buyer’s quality team checks at the destination port.
The in-process inspection frequency is typically every 10 to 50 parts for a 500-piece production batch, and the inspection tooling is typically a hand caliper for non-critical dimensions and a CMM for critical-to-quality dimensions. A supplier that documents the in-process inspection plan with a per-dimension inspection frequency is the supplier that has invested in the in-process envelope, and a supplier that documents “we will inspect every 50 parts” without a per-dimension inspection frequency is a step behind on the in-process envelope. The ASQ statistical process control and measurement system analysis reference is the industry-standard reference for the Cpk calculation, the control-chart envelope, and the gauge R&R (repeatability and reproducibility) study, and a supplier that documents the SPC envelope against the ASQ reference is the supplier that has invested in the SPC discipline.
The SPC envelope includes the control charts (X-bar and R charts for variable data, p-charts for attribute data), the Cpk values (the process capability index, with a target of Cpk ≥ 1.33 for a stable process and Cpk ≥ 1.67 for a high-capability process), and the out-of-control action plan (the procedure for investigating an out-of-control point, the procedure for stopping the production batch if the out-of-control point cannot be explained). A supplier that returns all three SPC components is the supplier that has invested in the SPC envelope, and a supplier that returns only a control chart without Cpk values is a step behind on the SPC envelope. The ISO 9001:2015 quality management standard defines the SPC envelope, and a supplier with a current ISO 9001:2015 certificate is the supplier that has invested in the SPC envelope.
Step 8: Final Inspection, Traceability, and Shipping Documentation
The eighth step is the final inspection, traceability, and shipping documentation, and the deliverable from this step is a documented final-inspection report (every critical-to-quality dimension measured on the CMM, with a pass/fail status), a documented traceability chain (mill → incoming-inspection → CNC machine → CMM → shipping dock), and a documented shipping package (commercial invoice, packing list, certificate of origin, compliance certificate, MTC). The final-inspection report is the document that the buyer’s receiving quality team checks at the buyer’s incoming-inspection bench, and the shipping package is the document that the buyer’s customs team checks at the destination port.
The traceability chain is the second component of the step, and the traceability chain is the document that the buyer’s quality team uses to recall a specific production batch in the event of a destination-port failure. The traceability chain includes the mill heat number, the supplier’s incoming-inspection lot number, the supplier’s CNC machine identifier, the supplier’s CMM program identifier, the supplier’s CMM inspection date, the supplier’s shipping date, and the supplier’s invoice number. A supplier that returns all seven components of the traceability chain is the supplier that has invested in the traceability envelope, and a supplier that returns only the mill heat number is a step behind on the traceability envelope.
The shipping package is the third component of the step, and the shipping package includes the commercial invoice (the part description, the quantity, the unit price, the total price, the currency, the incoterms), the packing list (the carton count, the part count per carton, the carton weight, the carton dimensions), the certificate of origin (the country of origin, the supplier’s signature, the chamber-of-commerce stamp if required), the compliance certificate (the ISO 9001:2015 certificate for general quality, the IATF 16949:2016 certificate for automotive, the ISO 13485:2016 certificate for medical device), and the MTC (the mill test certificate for the raw material lot). A supplier that returns all five components of the shipping package is the supplier that has invested in the shipping-package envelope, and a supplier that returns only the commercial invoice and the packing list is a step behind on the shipping-package envelope.
Supplier Evaluation Grid: The 8-Criterion Scorecard
The 8-criterion supplier evaluation grid that an OEM or a tier-1 supplier applies to a custom CNC machined part or a special-drawing assembly is: (1) drawing review and manufacturability, (2) material certification and incoming inspection, (3) tooling, fixture, and work-holding, (4) machine-tool envelope and calibration, (5) CMM inspection and ISO 10360 accuracy, (6) first-article inspection report, (7) in-process inspection and SPC, and (8) final inspection, traceability, and shipping documentation. A supplier that passes all 8 criteria with documented deliverables is the supplier that the procurement team shortlists to two or three candidates, and the supplier that passes 6 or 7 criteria is held as a second-source option. The supplier that passes 5 or fewer criteria is removed from the comparison regardless of price, lead time, or capacity.
The 8-criterion grid is the procurement reference for the 2026 custom CNC machined part sourcing program, and the grid’s deliverable is a 2-to-3-supplier shortlist with a documented side-by-side comparison on the 8 criteria. The supplier-evaluation grid that an OEM or a tier-1 supplier builds against the 8 criteria is the path to a 50-piece to 5,000-piece production batch of a custom machined part or a special-drawing assembly with a destination-port quality envelope that holds at the ISO 9001:2015 / ISO 13485:2016 / IATF 16949:2016 regulatory destination.
For procurement teams that want a documented 8-criterion evaluation of FRIMA’s CNC machining and quality-control envelope, the CNC Milling Service page lists the machine-tool inventory and the material range, the quality-control page documents the CMM and traceability stack, and the Contact FRIMA for a Quote page is the entry point for a 24-hour first-article review. The engineering team returns the manufacturability review, the CMM inspection strategy, and the lead-time estimate within one business day of the request-for-quotation, and the first-article CMM inspection report is delivered within 5 business days of the first-article sample being cut.
Engage HAOCHU on your 2026 custom casting and CNC program
Sourcing a custom CNC machined part to a special-drawing spec and need a Ningbo-based supplier with documented pre-production CMM inspection, a process-FMEA-ready engineering team, and a PPAP-style first-article report for each production batch? Review the CNC milling service page for the machine-tool envelope and material range, the quality-control page for the CMM and traceability stack, and the contact FRIMA for a quote page to submit a 2D / 3D drawing for a 24-hour first-article review and a documented CMM inspection plan. The engineering team returns the manufacturability review, the CMM inspection strategy, and the lead-time estimate within one business day of the request-for-quotation.
FAQQ1: What is the difference between a CMM and a hand caliper for first-article inspection?
A1: A CMM (coordinate measuring machine) is a precision measurement instrument that measures dimensions in three-dimensional space with an accuracy of 1.5 to 5 μm, depending on the CMM class. A hand caliper is a portable measurement instrument that measures linear dimensions with an accuracy of 20 to 50 μm. The CMM is required for critical-to-quality dimensions, and the hand caliper is acceptable for non-critical reference dimensions. A first-article report that uses only a hand caliper for all dimensions is a first-article report that is not compliant with a tier-1 customer’s quality envelope.
Q2: What is the ISO 10360 accuracy class for a tier-1 CMM?
A2: The ISO 10360 accuracy class for a tier-1 CMM is MPE = 1.5 + L/333 μm, where L is the measured length in mm. This means that a 100 mm dimension has an accuracy envelope of 1.5 + 100/333 = 1.8 μm, and a 1,000 mm dimension has an accuracy envelope of 1.5 + 1,000/333 = 4.5 μm. A supplier that returns an ISO 10360 certificate with MPE = 1.5 + L/333 μm is the supplier that has invested in the CMM accuracy envelope. A supplier that returns only “CMM calibrated” without an ISO 10360 certificate is a step behind.
Q3: What is a PPAP-style first-article report, and when is it required?
A3: PPAP (production part approval process) is the AIAG reference for the automotive industry, and a PPAP-style first-article report includes the dimensional inspection report, the material certification, the functional test report, the appearance report, and the control plan. A PPAP-style report is required for an automotive tier-1 customer, and it is the procurement reference for any customer that requires a documented production-batch approval process. A supplier that returns a PPAP-style report is the supplier that has invested in the first-article envelope, and a supplier that returns only a dimensional inspection report is a step behind.
Q4: What is the difference between ISO 9001, ISO 13485, and IATF 16949 for a CNC machining supplier?
A4: ISO 9001:2015 is the general quality management standard that applies to any industry, and a CNC machining supplier with an ISO 9001:2015 certificate is the baseline. ISO 13485:2016 is the medical device quality management standard, and a supplier with an ISO 13485:2016 certificate is qualified for medical-device production. IATF 16949:2016 is the automotive quality management standard, and a supplier with an IATF 16949:2016 certificate is qualified for automotive production. A supplier with all three certificates is qualified for the medical-device and automotive destination markets, and a supplier with only ISO 9001:2015 is qualified for the general industrial destination market.
Q5: What is the Cpk value that a tier-1 supplier targets for a CNC machined part?
A5: The Cpk value that a tier-1 supplier targets for a CNC machined part is Cpk ≥ 1.33 for a stable process and Cpk ≥ 1.67 for a high-capability process. A Cpk of 1.33 means that the process spread is 4 sigma inside the specification limit, and a Cpk of 1.67 means that the process spread is 5 sigma inside the specification limit. A supplier that returns a documented Cpk value for each critical-to-quality dimension is the supplier that has invested in the SPC envelope, and a supplier that returns only a control chart without Cpk values is a step behind.
About Us
General Manager at Ningbo FRIMA Industry Co., Ltd
Frank Kann is the General Manager at Ningbo FRIMA Industry Co., Ltd, with 15+ years of experience in custom machined parts, CNC machining parts, special drawing parts, fabrication, and assembly mechanism. His expertise covers CNC machining, special drawing production, fabrication, and project management. He leads the engineering team that runs the 8-step pre-production quality verification framework for FRIMA’s OEM customers, and the same CMM-backed first-article discipline that he applies to FRIMA’s medical-device and automotive-tier production programs is what he brings to every special-drawing custom machined part that enters the FRIMA production floor.
Media Contact
Company Name: Ningbo FRIMA Industry Co., Ltd.
Contact Person: Media Relations
Email: Send Email
Country: China
Website: https://www.frimaparts.com/


